
FieldMark Portable fixtures
Workholding with the right fixtures makes or breaks successful portable laser marking. Reliable, accurate results on site depend on fixtures that hold the part securely and repeatably for FieldMark Portable.
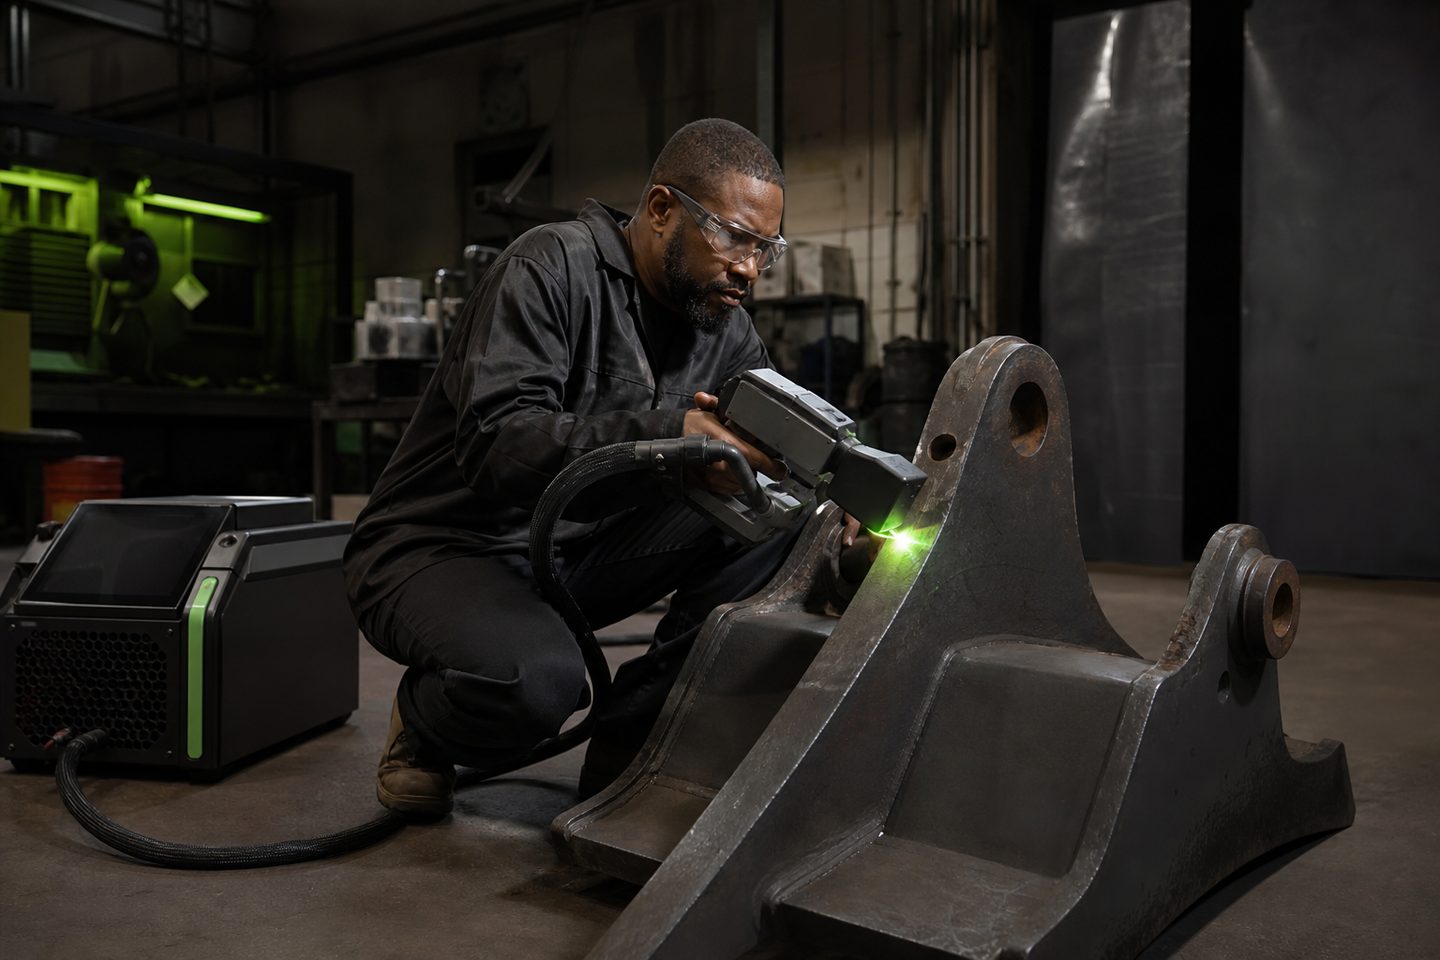
Browse materials, jaws, straps, and rotary kits.
- Flat fixture cues
- Rotary / clamp limits
- First-article photo notes
Also see beam notes and projects.
Why fixturing is key for reliable results
Whether you are marking asset tags on mining gear or serials on pipe flanges, how you clamp or jig the part has a direct impact on accuracy and repeatability. Poor fixturing lets parts move, causing blurred or misplaced marks, and can also lead to safety risks if the beam is misaligned.
A secure, stable fixture keeps the part exactly where you want it during marking. Repeat jobs depend on being able to return the part to the same position, especially for codes and regulatory marks. Good fixturing protects both the operator and the equipment from accidental slips or burns.
Fixture types for FieldMark Portable applications
FieldMark Portable is designed for flexibility on-site and in the workshop. The most common fixture types are screw or cam clamps (for flat plates and tags), V-blocks or V-jigs (for round shaft or pipe marking), and magnetic bases for ferrous parts.
Rotary chucks are available for occasional rotary marking on pipes and rods. For irregular or large parts, webbing straps and custom nest plates help hold the work steady. Always select a fixture that matches the surface and geometry of your part without crushing or distorting it.
- Screw clamps for flat items and tags
- V-blocks for round and oval work
- Rotary chucks for pipes and rods
- Magnetic bases on steel
- Straps or nest plates for large or awkward shapes
How to set up and check a fixture for first articles
Before you run production, make a first-article mark to check fixture alignment and clamping. A solid setup avoids wasted parts and inconsistent marks.
Take clear photos of your first-article setup, including clamp positions and any key datums. Mark these on your job sheet or nest brief for future reference. If you are working on a customer site, keep a record for traceability and repeat jobs.
- Clean part and fixture before clamping
- Check alignment with a visible pointer or guide beam
- Tighten clamps evenly, avoid over-tightening
- Confirm the part cannot move or vibrate
- Do a test mark in a safe area if possible
- Photograph the setup and note any special cues
Common fixture faults in autofeed cutting and how to prevent them
A loose or uneven clamp is the quickest way to spoil a mark. Watch for soft jaws or worn-out straps that let parts slip, especially after moving FieldMark between sites. Never use PVC material for fixtures, it can release corrosive fumes if hit by the beam.
Avoid clamping too close to the marking area, as metal jaws can reflect the laser and damage the optics or cause stray marks. For rotary work, check that the part is centred and spins smoothly before marking. Keep your fixtures clean and inspect them for wear at the start of each job.
- Never use soft, flammable or PVC fixtures near the beam
- Double-check part stability before marking
- Keep jaws and plates clean and free of burrs
- Replace straps and clamps that show wear
- Position clamps outside the marking field
What our Fibre Laser customers say
Verified Google reviews
